Choosing the best medical diagnostic parts in China starts with understanding the equipment, not browsing a supplier catalogue. A connector, sensor, pump, or precision-machined housing can affect fit, measurement stability, and maintenance. Small differences matter. A sensor that drifts under repeated use may create avoidable service work, even when its initial test looks acceptable. Buyers need clear specifications, consistent production, and reliable communication.
How to select parts for medical diagnostic equipment is therefore not a price-only question. Compare materials, tolerances, operating conditions, and expected service life against the equipment’s documented requirements. Ask suppliers how they control incoming materials and production changes. Request relevant inspection records, test results, and traceability information, then verify that the documents match the exact part and revision. A polished brochure is not enough. Samples should be evaluated under realistic conditions, including assembly fit and repeated operation where appropriate.
Experience also means noticing what remains uncertain. A supplier may answer quickly but provide limited detail about process controls; that deserves follow-up, not an immediate rejection. Review communication, sample quality, production capacity, and after-sales support together. Confirm who handles design changes and how deviations are reported. No checklist removes every risk. But a documented, evidence-based comparison can help buyers make a more dependable choice and build a sourcing relationship that supports equipment quality over time.
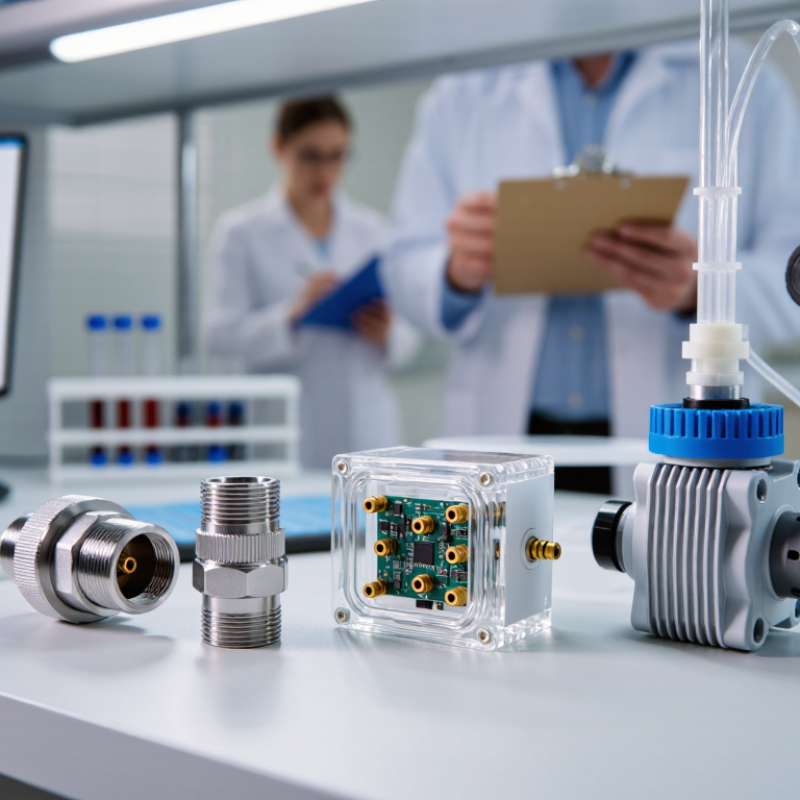
Start with the clinical task, not a parts catalogue. Specify what the device measures, which sample it handles, and where it will be used. A bedside analyzer may face dust, movement, and frequent cleaning; a laboratory instrument may need stable temperature control.
Small details matter. Define acceptable accuracy, repeatability, response time, and measurement range before comparing components. A sensor that meets a headline accuracy figure may still drift during long runs or perform poorly with real patient samples.
Turn these needs into testable requirements: dimensions, power limits, connectors, operating temperature, and expected service life. Check how each part fits the full device, including software interfaces and calibration steps. Ask suppliers in China for drawings, material specifications, test records, and traceability information.
Review a sample under realistic conditions, not only on a clean bench. A specification sheet is useful, but it can leave gaps. For example, a connector may fit yet loosen after repeated handling. Record unresolved questions and agree on acceptance tests before ordering.
Clinical performance must be verified in the finished device; component data alone cannot prove it.
Choosing medical diagnostic parts starts with the exact equipment model, revision, and intended function. Record the part number, dimensions, connector type, pinout, operating voltage, and signal range. A plug may fit yet carry the wrong signal. Check drawings and tolerances, not just product photos. Small mismatch, major trouble.
Material choice depends on where the part sits. For patient-contact or fluid-path components, verify material composition, cleaning method, and resistance to disinfectants. For electronic parts, check heat limits, insulation, shielding, and expected service life. Ask suppliers for traceable specifications and test records. Grand View Research’s Medical Devices Market report estimated the global market at US$518.5 billion in 2023, reflecting a large and varied supply chain. That scale makes careful specification important, but market size does not prove a component is suitable. Compare the part against the equipment manufacturer’s service documentation and applicable technical standards. A neat spec sheet is not proof of fit. Supplier drawings can omit tolerances, so confirm critical dimensions on a sample before ordering in volume.
Choosing medical diagnostic parts in China depends on more than a low quotation. Match the supplier’s process to the part’s function: molded housings need stable dimensions, while machined fittings need consistent surfaces and tolerances. Ask how equipment is maintained, how parts are inspected, and how process changes are controlled. Request sample inspection records and lot traceability details. For critical dimensions, compare measured results with your drawing, not a general “passed” note. Small gaps matter.
Tips: Arrange a production review, in person or remotely. Check calibration labels, incoming-material checks, and work instructions near the line. Compare a pilot batch with later production; one good sample proves little. Ask who approves deviations and how issues are reported.
Judge capability by evidence, not polished presentations. Check whether operators are trained and inspection tools suit your tolerance range. Discuss production capacity, outsourced steps, and backup plans before launch. Clear answers build confidence. Still, audits have blind spots, and a certificate cannot prove every batch is consistent. Set written acceptance criteria, retain approved samples, and review early shipments closely. Revisit your checklist after the first production run; routine problems may only appear at scale.
When sourcing medical diagnostic parts in China, verify the quality system at the production site, not only the supplier’s sales office. Request a current ISO 13485 certificate and match its legal entity, factory address, scope, and expiry date with the certification body’s records. ISO’s 2022 Survey reported 31,481 ISO 13485 certificates across 106 countries and economies. This shows wide adoption, not that every certified part is suitable for your device. Paper is not proof.
Ask for recent audit findings, corrective-action records, and traceability examples linking a component lot to inspection results. Check that measuring equipment is calibrated and that changes to materials or processes require documented approval. Verify applicable NMPA registration or filing for products marketed in China, then check the rules for your destination market separately. For US sales, FDA establishment registration or device listing does not itself mean FDA approval or clearance. A polished PDF can be misleading. I would still check the factory, though a rushed audit can miss problems; that limitation deserves attention. Also confirm that certificates cover the actual manufacturing activity, not just a nearby office or unrelated product scope.
| Evaluation dimension | What to verify | Evidence to request | Practical acceptance signal |
|---|---|---|---|
| Medical-device quality management system | Check whether the supplier’s quality system is certified to ISO 13485:2016 and whether the certificate scope covers the relevant manufacturing site and activities. | Current certificate, certification-body details, scope, covered site addresses, and the latest audit or surveillance status. | The certificate is current and its scope matches the actual site and processes used for the part. Verify it with the issuing body or relevant accreditation directory. |
| General quality certification | Determine whether ISO 9001 certification supports the supplier’s broader quality controls, while recognizing that it is not a substitute for ISO 13485 when medical-device quality controls are required. | Certificate, validity dates, covered locations, and defined scope. | The supplier explains how its quality system addresses the specific risks and documentation needs of the intended medical-device application. |
| China regulatory status and product classification | Clarify the intended use and determine whether the finished diagnostic device is subject to NMPA registration or filing requirements. A component does not automatically require a separate NMPA registration; requirements depend on its role and applicable rules. | Where applicable, the finished-device registration or filing information, product classification rationale, and documents showing how the component supports the device manufacturer’s compliance work. | The supplier does not claim that a component certificate alone authorizes the finished diagnostic device for sale in China. Regulatory responsibilities are clearly assigned. |
| Target-market regulatory support | Confirm the evidence needed for the intended market. For the EU, assess the finished device against applicable Medical Device Regulation (EU) 2017/745 requirements. For the US, confirm applicable FDA requirements, including establishment registration and device listing where required. | Relevant declarations, technical data, test reports, traceability records, and written clarification of the supplier’s role in the finished-device compliance process. | The supplier distinguishes component-level evidence from finished-device authorization. FDA registration or listing is not the same as FDA approval. |
| Risk management and design controls | Check how design or process changes are assessed for their effect on safety, performance, and the finished device’s risk controls. ISO 14971 is a commonly used medical-device risk-management standard. | Risk-related input, design or process review records where relevant, specifications, validation evidence, and documented change-control procedures. | Risks and changes are documented, reviewed, and communicated to the customer before implementation when they could affect the part or finished device. |
| Manufacturing process control | Review control of critical production steps, equipment, inspection criteria, nonconforming product, corrective actions, and process validation where output cannot be fully verified by later inspection. | Process flow, control plans, inspection records, validation reports where applicable, calibration records, and corrective-action examples with sensitive details removed. | Critical characteristics have defined acceptance criteria, records are retained, and corrective actions address root causes rather than only the immediate defect. |
| Test and measurement capability | Confirm that inspection methods are suitable for the part’s critical dimensions or performance characteristics and that measuring equipment is maintained and calibrated. | Test methods, sample reports, equipment calibration records, and, for external testing where relevant, the laboratory’s ISO/IEC 17025 accreditation scope. | Reports identify the tested item, method, results, acceptance limits, and date; the laboratory scope covers the test being relied upon. |
| Materials and chemical compliance | Identify materials that may affect safety, biocompatibility, chemical restrictions, or diagnostic performance. Apply requirements such as RoHS or REACH only where relevant to the product and target market. | Material specifications, supplier declarations, test reports where needed, and change notifications for material or sub-supplier changes. | Evidence is specific to the supplied part and material; generic declarations are supported by traceable information when requested. |
| Cleanroom and contamination controls | If cleanliness or particle control matters to the part, verify the relevant environmental controls and whether any claimed cleanroom classification is maintained under ISO 14644 requirements. | Cleanroom classification and monitoring records, cleaning procedures, gowning controls, and evidence that the specified area is used for the relevant production step. | Environmental controls match the product’s documented needs; a cleanroom claim is supported by current, site-specific records. |
| Sterilization, if applicable | For parts supplied sterile or exposed to a sterilization process, verify that the process and product compatibility are assessed using applicable standards, such as ISO 11135 for ethylene oxide, ISO 11137 for radiation, or ISO 17665 for moist heat. | Sterilization validation and routine-control records, packaging information, and evidence supporting the claimed sterile condition and shelf life, where relevant. | The sterilization method, validation responsibility, packaging configuration, and release criteria are clearly defined. Do not assume a part is sterile unless specified and supported by evidence. |
| Traceability and change notification | Assess whether parts can be traced to relevant production lots, materials, and manufacturing records, and whether the supplier notifies the customer of changes that could affect form, fit, function, or compliance. | Sample batch or lot records, labeling examples, retention policy, sub-supplier controls, and a documented change-notification agreement. | Traceability is defined in advance and records can be retrieved within an agreed timeframe; material, site, process, and sub-supplier changes are controlled. |
| Supplier audit and ongoing performance | Evaluate the actual manufacturing site, not only the sales office. Review quality performance, complaint handling, delivery consistency, and corrective-action responsiveness. | Remote or on-site audit findings, quality metrics with defined periods and denominators, complaint and corrective-action procedures, and an escalation contact. | Findings are addressed with documented corrective actions, and performance data is specific, current, and reviewed periodically. |
Note: Applicable obligations depend on the part, intended use, finished-device classification, and target market. Confirm regulatory requirements with the responsible finished-device manufacturer and qualified regulatory personnel.
A low unit price can hide the real cost. Compare quotes for identical specifications, quantities, inspection records, and packaging. Look beyond the quote. Include freight, insurance, taxes, payment fees, and any handling charges in your calculation. For example, a small sensor may need protective packaging that adds cost but reduces damage risk. Ask how rejected parts are replaced and who pays return shipping. A spreadsheet helps, though it can miss costs that appear only after an order is placed. Confirm every charge in writing.
Delivery terms deserve the same attention. Ask whether the quoted lead time means production completion or arrival at your facility. Request estimated dispatch and transit dates, tracking details, and clear procedures for delays or damaged shipments. For critical components, check whether the supplier can provide consistent batches and advance notice of shortages. After-sales support matters too. Confirm the warranty period, response hours, troubleshooting process, and availability of replacement parts. Ask for technical documents relevant to installation and compatibility, then check that support staff can answer practical questions. A quick reply is useful, but a clear, documented solution is better. Some details may still be uncertain, so record assumptions before committing.
Compare total cost, delivery terms, and after-sales support before making a purchasing decision.
How to use this chart: These suggested weights are a planning framework, not industry averages. Compare each supplier’s landed cost, confirmed delivery terms, and documented after-sales support, then adjust the weights to fit your requirements. Include shipping, duties, and other applicable charges when calculating total cost.
Specify the measurement, sample type, and intended setting. Set accuracy, repeatability, response time, and measurement range. A bedside unit may face dust and frequent cleaning.
A sensor may drift during long runs or perform differently with patient samples. Test it in the finished setup, not only on a clean bench.
Record the equipment model and revision, part number, dimensions, connector, pinout, voltage, and signal range. A plug can fit. Still wrong.
Confirm material composition, cleaning methods, and resistance to disinfectants. For electronic parts, check heat limits, insulation, shielding, and service life.
Request drawings, material specifications, test records, and traceability details. Agree on written acceptance tests before ordering. A spec sheet can leave gaps.
Compare measured results with your drawings and tolerances. Review inspection records, calibration labels, incoming-material checks, and work instructions.
Ask about outsourced steps, process changes, deviations, and backup plans. Compare a pilot batch with later shipments. One good sample proves little.
No. Verify clinical performance in the finished device, including software interfaces and calibration steps. I may be overcautious, but certificates cannot prove every batch.
Choosing the right components for medical diagnostic equipment starts with a clear understanding of the device’s technical specifications, clinical purpose, operating environment, and performance requirements. Define the functions each part must support, then identify suitable materials, dimensions, electrical or mechanical interfaces, and compatibility needs. This careful planning helps reduce integration problems and supports reliable, consistent diagnostic performance.
When considering suppliers in China, assess their engineering expertise, production capacity, process controls, and ability to provide technical documentation and samples. Verify relevant quality management systems, certifications, and regulatory documentation for the intended market. Compare the total cost of ownership rather than unit price alone, taking into account testing, packaging, shipping, lead times, and potential maintenance needs. Clear delivery terms and dependable after-sales support are also essential. A structured approach to How to select parts for medical diagnostic equipment can help buyers make informed decisions while balancing quality, compatibility, cost, and long-term supply reliability.
Xinli Technology